
1-805-484-2992
Quotes - Engineering - SalesU-Tube Heat Exchangers For
Surface Finish, Polish and Passivation
U-Tube Duty
Roughness is a cleaning specification. A rough surface holds soil in valleys that cleaning solution flows over rather than through, and gives biofilm somewhere to anchor.
Ra is the arithmetic average deviation of the surface profile, measured in microinches. Lower is smoother. On sanitary work, 32 Ra on product contact and 40 Ra on exterior surfaces are the numbers most specifications settle on.
Mechanical polishing. Progressive abrasive work to a target roughness. It is economical and effective, and it can smear metal over small defects and occasionally embed abrasive particles.
Below 32 Ra, Consistency Beats the Number. Cleanability improves as roughness falls, and the returns diminish. Below about 32 Ra the practical benefit comes more from uniformity and freedom from defects than from a lower average.
A surface at 20 Ra with a scratch, a fold or a patch of heat tint is worse in service than a consistent 32 Ra surface with none of those. Specify what will be verified and verify it.
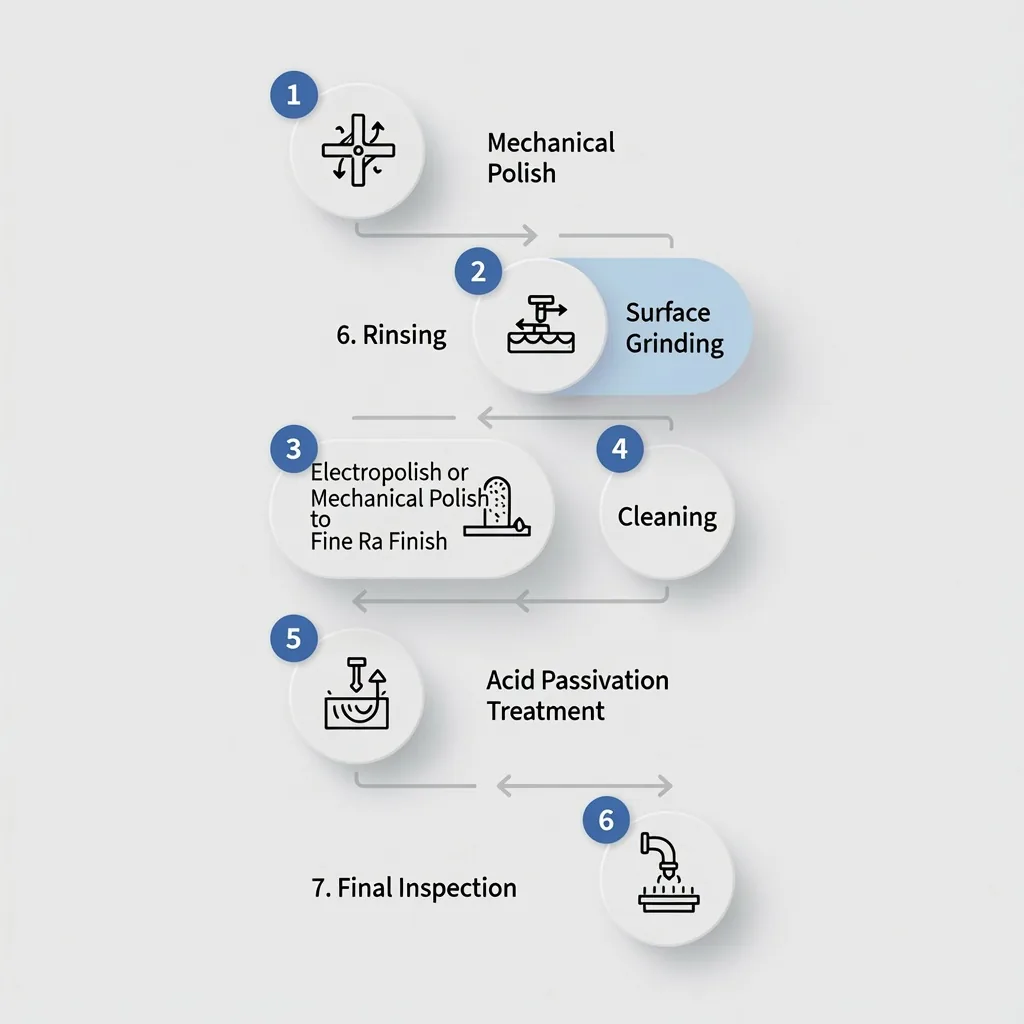
Passivation. A chemical treatment removing free iron and encouraging the chromium oxide layer to reform. It is a distinct step from polishing, and it is required after fabrication regardless of how the surface was finished.
Request a Quote
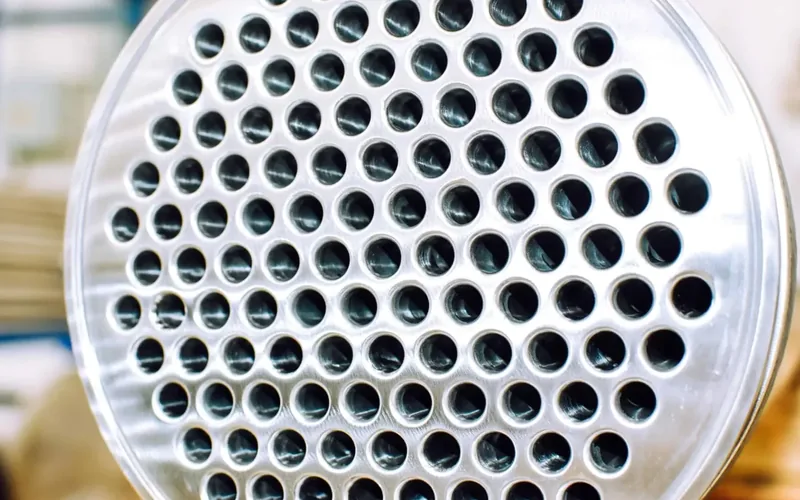
Roughness, Polish and Passivation
Ra is the arithmetic average deviation of the surface profile, measured in microinches; lower is smoother. Roughness is a cleaning specification, because a rough surface holds soil in valleys that cleaning solution flows over rather than through. Below about 32 Ra the practical benefit comes more from uniformity and freedom from defects than from a lower average.
Roughness Targets
Polishing Methods
Passivation
Related
MATERIALS & FINISHES • DESIGN
304L & 316L Stainless
Where each fits, and the chloride cracking limit.
+ Learn More
MATERIALS & FINISHES • DESIGN
Carbon Steel
Shells, tubes, corrosion allowance and coatings.
+ Learn More
MATERIALS & FINISHES • DESIGN
Duplex & High Alloys
2205, Alloy 20, Hastelloy and how each bends.
+ Learn More
