
1-805-484-2992
Quotes - Engineering - SalesU-Tube Heat Exchangers For
ASME BPE Requirements
U-Tube Duty
BPE is the standard that makes an exchanger qualifiable. It governs the things a validation engineer has to prove and a pressure code says nothing about.
The Bioprocessing Equipment standard was created because pressure vessel codes address containment and say nothing about cleanability, drainability or traceability. BPE fills that gap with requirements specific enough to be verified and documented.
Surface designations. The SF series specifies both a roughness limit and the finishing method, distinguishing mechanically polished from electropolished surfaces. That distinction matters because the two behave differently in hot high-purity service.
Documentation Cannot Be Retrofitted. Weld maps are produced as welds are made. Traceability survives only if it is maintained through cutting and forming. Finish verification happens while surfaces are accessible.
None of that can be reconstructed afterward with any credibility. Tell us at quotation what your IQ and OQ protocols require, so it becomes part of the fabrication plan rather than a problem discovered during qualification.
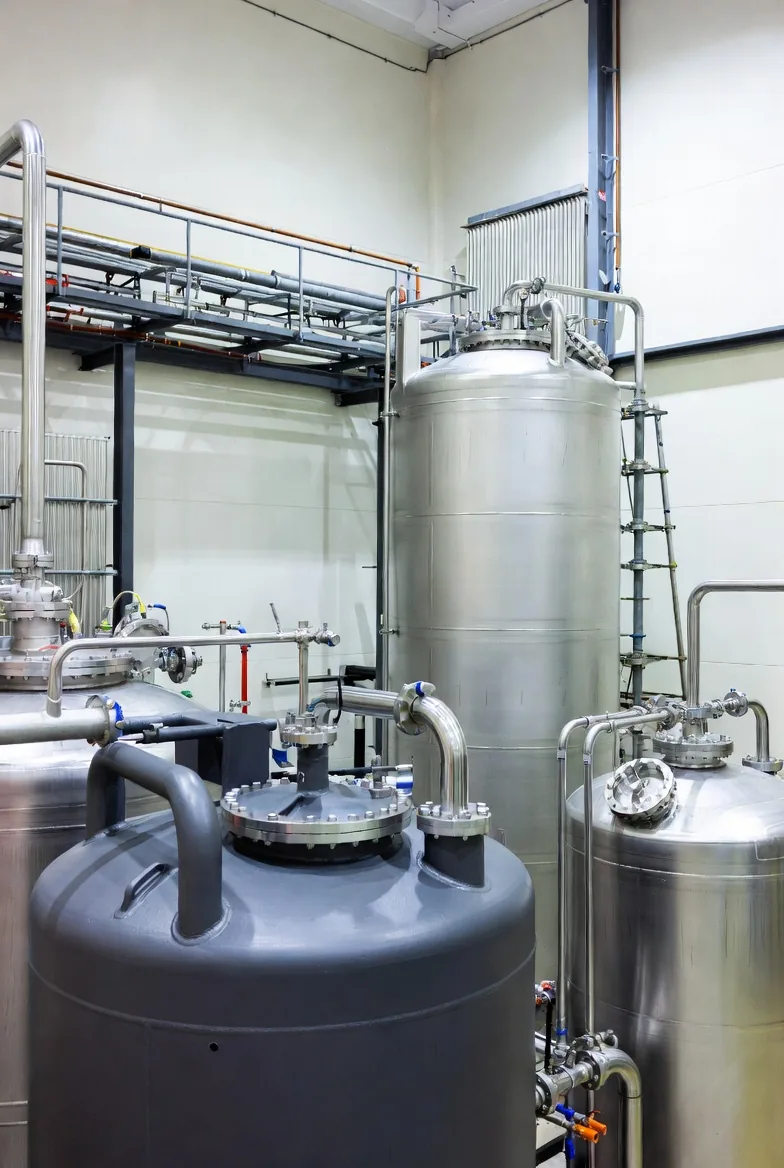
Dead legs, slope and traceability. Projections limited by length-to-diameter ratio, drainability in the installed orientation, and material traceability running from mill certificate through to the nameplate.
Request a Quote
What BPE Adds to a Pressure Code
Pressure vessel codes address containment and say nothing about cleanability, drainability or traceability. BPE fills that gap with requirements specific enough to be verified and documented, which is what makes an exchanger qualifiable. None of it can be reconstructed after fabrication, so the protocol requirements have to be part of the quotation.
Surface Designations
Geometry
Documentation
Related
CODES & STANDARDS • DESIGN
ASME Section VIII
The U-stamp, the U-1 data report and the hydro test.
+ Learn More
CODES & STANDARDS • DESIGN
TEMA Classes R, C & B
Classes R, C and B, and how the choice moves price.
+ Learn More
CODES & STANDARDS • DESIGN
3-A Sanitary Standards
Scope, symbol authorization and verification.
+ Learn More
